Skip to content
Capabilities

One works. Every discipline.

Engineering review, design, fabrication, welding, inspection and testing under one roof in Ankleshwar — with two specialities our customers return for.

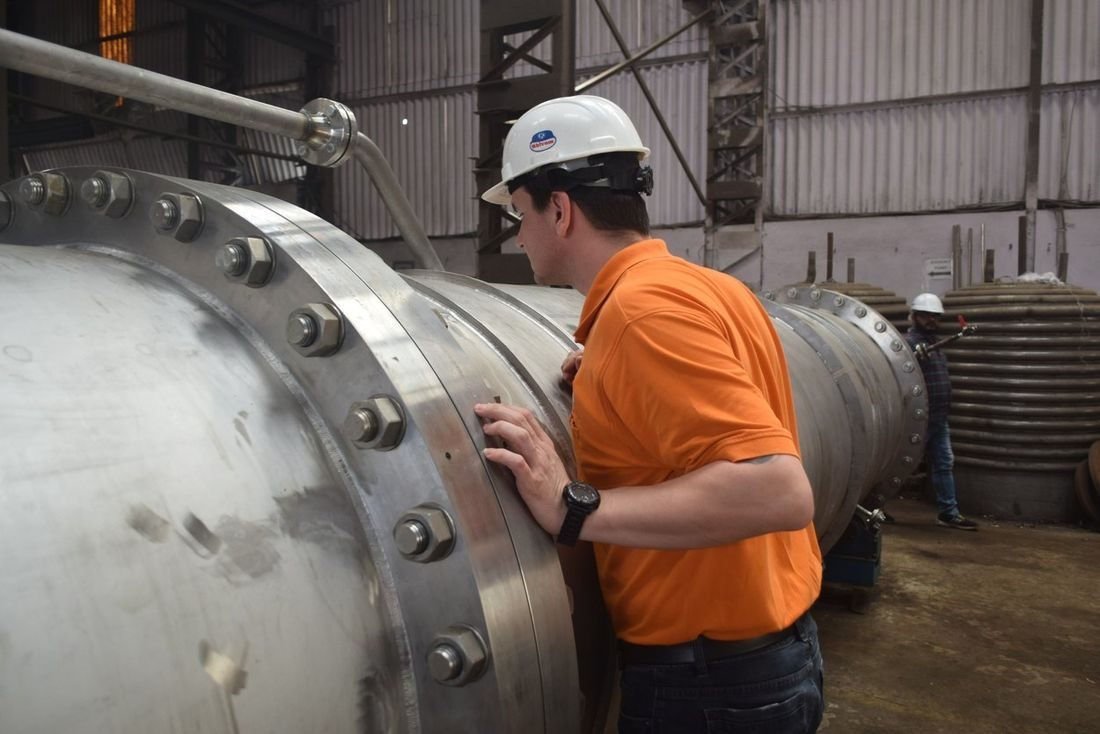
Internal coils inside a polished alloy vessel Speciality High & exotic alloys Hastelloy, Inconel, Monel, duplex and more — solid or explosion-bonded clad. Hydrogenator ready for dispatch Speciality Hydrogenator masters High-pressure hydrogenators, gas-induction reactors and autoclaves. Hydrofoil impeller inside a coil-fitted reactor Speciality Agitator assembly & impeller design Impellers sized for the duty, drives and seals matched to the vessel, trial-run before dispatch. Tube sheet of a shell and tube exchanger Speciality Shell & tube heat exchangers Every TEMA type — thermal design and rating with HTRI, mechanical design to TEMA and ASME, built to the tube.
Engineering review

Built to the drawing. Reviewed beyond it.

Typical points we raise during drawing review — every one goes to the customer for approval.

Process & performance
  • Heat-transfer area and jacket / limpet / coil layout
  • Agitator, baffle and coil interaction
  • Sparger and dip-pipe geometry
  • Drainability and dead zones
Maintenance & access
  • Manhole and handhole size and orientation
  • Removable internals and inspection access
  • Seal, gearbox and drive serviceability
  • Lifting, rigging and handling points
Operability & usability
  • Nozzle orientation for piping and instruments
  • Sight / light glass and sampling points
  • Platform, ladder and operating clearances
  • Cleaning, CIP and changeover needs
Safety & life cycle
  • MOC compatibility and corrosion allowance
  • Relief, vent and drain provisions
  • Weld-joint efficiency and NDT scope
  • Transport envelope and site erection
Design & engineering

Designed to the code — and to the process.

Mechanical and process design follow the applicable codes and your specification. Calculations are prepared and verified in Codeware COMPRESS and Intergraph PV Elite, heat-exchanger thermal design and rating with HTRI; drawings, 3D models and CNC programs in AutoCAD and SOLIDWORKS.

AutoCAD SOLIDWORKS 3D SOLIDWORKS CAM SOLIDWORKS Simulation Codeware COMPRESS Intergraph PV Elite
ASME BPVC Sec. VIII Divisions 1 & 2
EN 13445 · PD 5500 Unfired pressure vessels
TEMA Classes B, C & R
API 650 · IS 803 Storage tanks
IBR 1950 Indian Boiler Regulations
AD 2000 Merkblatt series
PED 2014/68/EU CE marking, Modules G & A2
ATEX EN ISO 80079 · EN IEC 60079
IS · DIN · BS National standards
ASME Sec. IX Welding qualifications
Manufacturing & welding

Workmanship you can measure.

Skilled welders, fitters and riggers; welding procedures, PQRs and welders qualified to ASME Section IX; welding quality controls to EN ISO 3834-2. Specialists in high-nickel alloys, duplex grades and stainless steels for corrosive and high-temperature service.

Our assembly facility runs agitator trials — varying speeds, balancing, air runs, hydrostatic tests and alignment.

GTAW
TIG and pulse-TIG
SAW
Column boom and rotators
SMAW
Qualified to ASME IX
TIG welding on a stainless vessel
TIG welding
Lip-type nozzle set-up
SAW column boom welding machine
SAW column boom
Inspection, QC & NDE

Traceable at every stage.

  1. 01 Raw materialTesting, identification and marking; traceability from receipt.
  2. 02 Fit-up & weldingQualified WPS / PQR and welders (ASME IX); EN ISO 3834-2 controls.
  3. 03 Stage inspectionHold and witness points per the approved ITP and QAP.
  4. 04 Heat treatment & NDTRT, UT, PT, MT and VT by in-house ASME NDE Level II personnel (ASME V / ISO 9712).
  5. 05 Testing & PMIHydrostatic / pneumatic testing; PMI on every finished item.
  6. 06 DossierTraceability records, inspection reports and test results.
Hydrostatic test bay Third-party stage inspection of a column
How we keep improving: lessons from every inspection feed our procedures — samples for each U-bend radius before production, equal attention to pressure and non-pressure parts, 100% visual checks at painting and pre-dispatch, and every verbal change documented with client approval.
Calibrated instruments in-house: bore gauges, micrometers and verniers to 600 mm, digital tongue tester, non-contact tachometer, X-ray film viewer, ultrasonic thickness gauge, densitometer, weld gauges and CAM-type master gauge, pressure gauges to 160 kg/cm²g, electrode baking oven to 400 °C, weighing machine to 300 kg, sound-level and lux meters.
Site services

At your plant, not only in ours.

Our ASME ‘U’ and National Board ‘R’ authorizations cover shop and field sites, so the same teams that build the equipment can support it on site — whether or not a project is running with us, and for equipment from our works or elsewhere. Service & support →

Installation & commissioning support Supervision of erection, alignment and trial runs for the equipment we supply.
Repairs & alterations Code repairs and alterations under our National Board ‘R’ certificate, at shop or field locations.
Maintenance & upgrades Agitator, seal and internals upgrades, re-tubing and modifications to equipment already in service.
Infrastructure & machinery

A self-sufficient works, expanded in 2023.

65,000+ sq ft
Unit 1 (Plots 5013–5016) and Unit 2 (Plot 5718)
40 t
Electric overhead cranes, plus 7.5 t rail crane
45 mm
Plate rolling up to 45 mm × 2,500 mm
8 m
Shed heights of 6.5 m and 8 m
CNC plasma cutting
CNC plasma cutting
3-axis CNC VMC
3-axis CNC VMC
Hydraulic plate rolling
Radial drilling
Radial drilling
Grinding, buffing & polishing
Electrode baking & holding

People: ~25–28 engineering & staff · ~52–55 skilled welders, fitters & machinists · ~28–30 support workers. Utility: 250 kVA DG set, compressors.